Thank you for writing to us. One of our executive will reach back to you through your submitted medium. In case there’s an urgency, feel free to connect over WhatsApp for faster response.
Prefer calling? Dial +919405982683 (International callers) or +919405982683 (Indian callers).
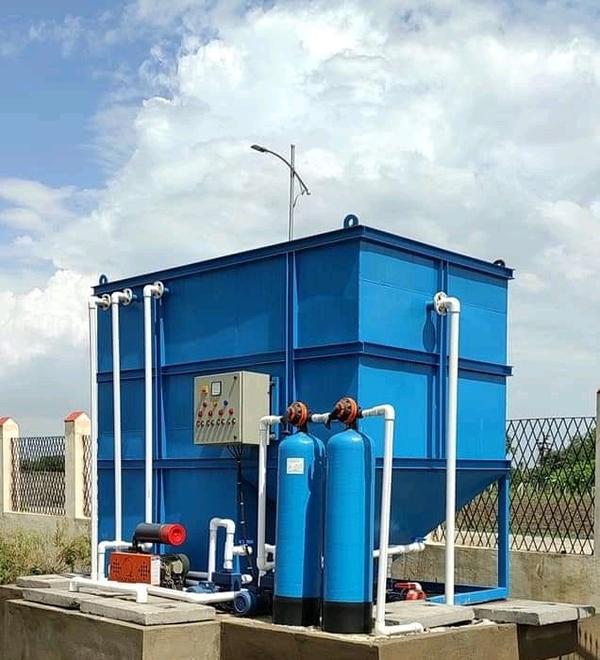
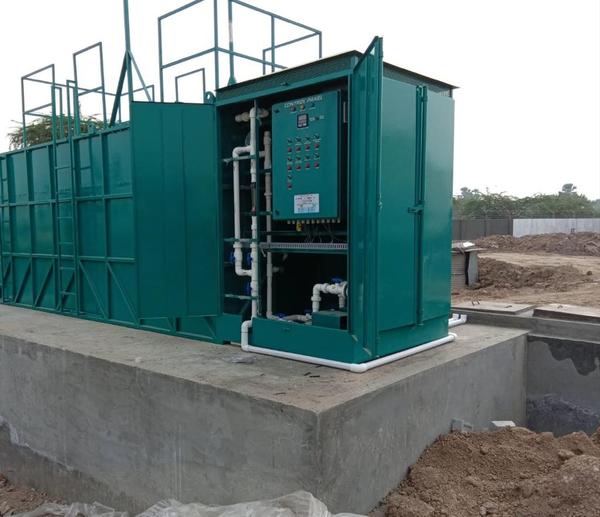
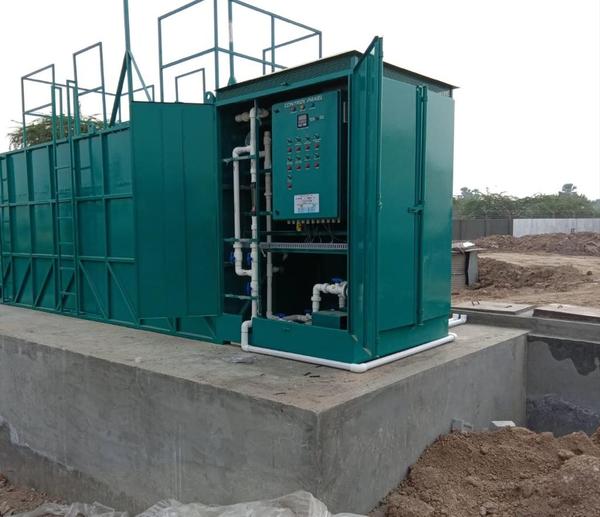
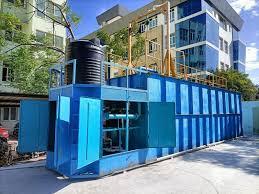
Modular sewage treatment plants are transforming the wastewater treatment industry by providing a flexible and efficient alternative to conventional STPs. These systems are pre-engineered, factory-built, and ready for on-site installation, reducing construction time and cost.
A modular STP plant is a compact, prefabricated, and scalable sewage treatment system that is built in a factory and then transported to the desired site for quick installation.
Key advantages of a modular STP
Quick installation: Since they are factory-built, modular units can be installed and commissioned in a matter of weeks, in contrast to the months required for conventional plants.
Space efficiency: Their compact footprint makes them ideal for locations with limited land, such as urban commercial buildings, hotels, and residential complexes.
Scalability: Modular designs allow for easy expansion by adding more units as wastewater treatment needs increase.
Cost-effectiveness: While the initial cost per unit may seem higher, modular STPs offer lower overall project costs due to reduced civil work, faster installation, and lower maintenance.
Portability: The units can be easily relocated, making them suitable for temporary projects or changing site requirements.
High reliability: Factory testing and standardized manufacturing ensure consistent and reliable performance.
Ease of operation: Many modular STPs feature automated control panels and remote monitoring, which simplifies operation and minimizes the need for on-site personnel.
Modular STPs are an excellent solution for a wide range of applications, including:
-Hotels, resorts, and hospitals
-Housing societies and residential complexes
-Small and medium-sized industrial units
-Schools and educational institutions
-Smart cities and temporary construction sites
-Decentralized wastewater treatment for smaller communities
A packaged sewage treatment plant (PSTP) is a compact, pre-engineered, and self-contained system designed to treat wastewater from domestic or industrial sources. It arrives pre-assembled and ready for installation, offering an efficient and more space-saving alternative to large, conventional treatment facilities.
Advantages
Packaged STPs are a modern wastewater management solution with many key benefits:
Compact design: Their small footprint makes them suitable for sites with limited space, such as residential complexes, hotels, and schools.
Rapid and easy installation: Since units are pre-fabricated and delivered ready-to-use, they can be installed and commissioned much faster than traditional plants.
Cost-effectiveness: PSTPs often have lower installation, operational, and maintenance costs due to their factory-built nature and advanced automated controls.
High efficiency: Many modern systems are designed for high treatment efficiency, often using a combination of anaerobic and aerobic processes to produce a high-quality effluent.
Environmental compliance: They help property owners and businesses meet strict environmental regulations and prevent the pollution of water bodies.
Water reuse: The treated water can often be reused for non-potable purposes like landscaping, flushing, or industrial processes, promoting water conservation.
Scalability: Their modular design allows for easy expansion or modification to accommodate increased wastewater volume in the future.
Common applications
PSTPs are a versatile solution for a wide range of decentralized wastewater needs:
-Residential complexes, townships, and housing societies
-Commercial buildings, hotels, and resorts
-Hospitals, schools, and other institutions
-Small-to-medium-scale industrial facilities
-Remote locations like villages, construction sites, and military bases
-Temporary installations for events or camps
-On-site treatment for properties not connected to a municipal sewer system
An MBR STP plant is a Sewage Treatment Plant that uses Membrane Bioreactor (MBR) technology to combine biological treatment with membrane filtration, producing high-quality, reusable treated water. The process involves microorganisms breaking down waste in a bioreactor and then passing the mixture through microfiltration or ultrafiltration membranes, which physically block suspended solids, bacteria, and pathogens, leaving behind clean water. MBR STPs are known for their compact design, ability to treat challenging wastewater, and production of high-quality effluent suitable for sensitive discharge or reuse applications.
Key advantages of MBR technology
Superior effluent quality: The membrane filtration produces very clean, clear, and virtually pathogen-free water that meets stringent environmental discharge standards. This high-quality water is also ideal for reuse in non-potable applications like irrigation, toilet flushing, and cooling towers.
Reduced footprint: MBR plants are significantly more compact, requiring 50–70% less space than conventional STPs because they eliminate the need for large, secondary clarifier tanks. This makes them ideal for urban areas with limited space.
Less sludge production: Due to the system's long sludge retention time, MBRs generate less excess sludge, which reduces disposal costs and handling requirements.
Modular and scalable design: The plants are modular, allowing for easy expansion as treatment capacity needs increase.
Automated operation: Advanced automation and monitoring reduce the need for constant on-site operator supervision, which lowers labor costs and ensures consistent performance.
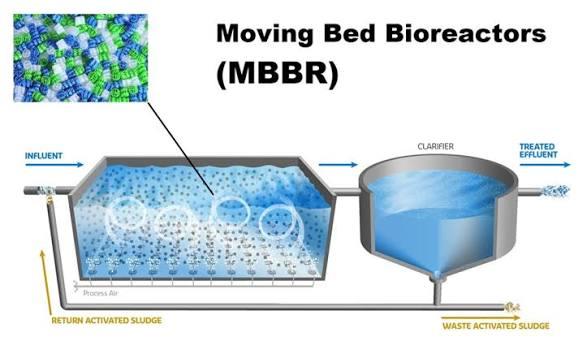
An MBBR STP is a Moving Bed Biofilm Reactor (MBBR) based Sewage Treatment Plant. This system uses a biological wastewater treatment process where microorganisms, which break down pollutants, grow on free-floating plastic carriers called bio-media.
How an MBBR STP works
Pre-treatment: Before entering the MBBR tank, wastewater goes through pre-treatment steps like screening and grit removal to protect downstream equipment.
MBBR biological treatment: Wastewater flows into an aeration tank filled with thousands of small, free-floating plastic media. An aeration grid supplies oxygen, which keeps the media in constant motion and provides oxygen for microbial growth.
Biofilm activity: Microorganisms attach to the surface of the bio-media and form a biofilm. This dense biofilm breaks down organic matter and other pollutants in the wastewater.
Clarification: After biological treatment, the water passes through a clarifier or settling tank. Retention screens at the tank outlet prevent the carrier media from leaving while allowing the treated water to pass. Any remaining solids are removed during this stage.
Disinfection: The final effluent may undergo additional polishing or disinfection before being discharged or reused.
Key components
Aeration tank/reactor: The primary basin where the biological treatment takes place and the carriers are suspended.
Bio-carrier media: Small, specifically designed plastic carriers, usually made from high-density polyethylene (HDPE), that provide a large surface area for biofilm growth.
Aeration system: Fine or coarse bubble diffusers supply oxygen to the microbes and keep the carriers moving within the tank.
Retention screens: Screens at the tank's outlet prevent the carrier media from escaping while allowing treated water to pass.
Clarifier: A tank for settling and removing any residual suspended solids after biological treatment.
Ozone is a very strong oxidant and virucide. The mechanisms of disinfection using ozone include: Direct oxidation/destruction of the cell wall with leakage of cellular constituents outside of the cell. Reactions with radical by-products of ozone decomposition.
Ozonation in wastewater treatment is an advanced oxidation process that utilizes ozone (O3) to disinfect and remove contaminants from wastewater. It's a powerful method for eliminating bacteria, viruses, and other pathogens, as well as oxidizing organic and inorganic substances that cause taste, odor, and color issues. Ozonation can be used as a standalone treatment or in combination with other methods like reverse osmosis or catalytic ozonation for enhanced purification.
How it works
Ozone Generation: Ozone is typically generated on-site at the wastewater treatment plant, often using a corona discharge method. This involves passing dry air or oxygen through a high-voltage electrical field, which converts stable oxygen molecules into ozone.
Ozone Diffusion: The generated ozone gas is then diffused into the wastewater, creating numerous tiny bubbles. This maximizes the contact area between the ozone and the contaminants in the water, facilitating the oxidation process.
Oxidation and Disinfection: Ozone, being a strong oxidizing agent, reacts with organic and inorganic pollutants in the wastewater. This process breaks down contaminants into simpler, less harmful substances like carbon dioxide and water. Ozone also effectively destroys microorganisms by damaging their cell walls and membranes, acting as a powerful disinfectant.
Applications in wastewater treatment
Ozonation finds application in various stages and aspects of wastewater treatment:
Disinfection: It effectively inactivates a wide range of pathogens including bacteria, viruses, and protozoa, reducing the risk of waterborne diseases.
Removal of Organic Pollutants: Ozone breaks down a wide array of organic compounds like pesticides, pharmaceuticals, and industrial chemicals that might be difficult to remove using conventional methods.
Color and Odor Removal: Ozonation eliminates unpleasant tastes, odors, and discoloration often caused by natural organic matter, according to Journal of Industrial Pollution Control.
Sludge Reduction and Dewatering: Ozonation can destroy filamentous bacteria that make sludge difficult to dewater, potentially reducing sludge volume and improving its handling characteristics.
Enhanced Biological Treatment: Ozone can improve the efficiency of subsequent biological treatment processes by increasing the biodegradability of organic matter.
Removal of Heavy Metals and other Inorganic Pollutants: Ozone oxidizes heavy metals like iron and manganese into insoluble forms that can be easily removed by filtration.
Benefits
High Effectiveness: Ozonation effectively removes a broad spectrum of pollutants and disinfects wastewater.
No Harmful Byproducts: Unlike some other disinfectants like chlorine, ozone decomposes rapidly into oxygen, leaving no toxic residuals in the treated water.
Enhanced Water Quality: It improves the aesthetic qualities of the water by removing color and odor.
Rapid Treatment: Ozonation typically requires shorter contact times compared to other disinfection methods.
Eco-friendly: Ozonation is considered a environmentally sound treatment option as it reduces the release of pollutants into the environment.
Future of ozonation in wastewater treatment:
Ongoing research focuses on improving the efficiency and cost-effectiveness of ozonation in wastewater treatment through:
Developing more efficient ozone generation technologies.
Optimizing ozone diffusion and contact methods.
Combining ozonation with other advanced treatment processes (e.g., Ozonation/Biological Treatment, Ozonation/Activated Carbon) to enhance overall contaminant removal and overcome the limitations of individual processes.
Exploring catalytic ozonation for increased efficiency and reduced cost.
In conclusion, ozonation offers a promising approach to improve wastewater treatment by providing effective disinfection, reducing a variety of pollutants, and contributing to the production of high-quality treated water that can potentially be reused or safely discharged into the environment.
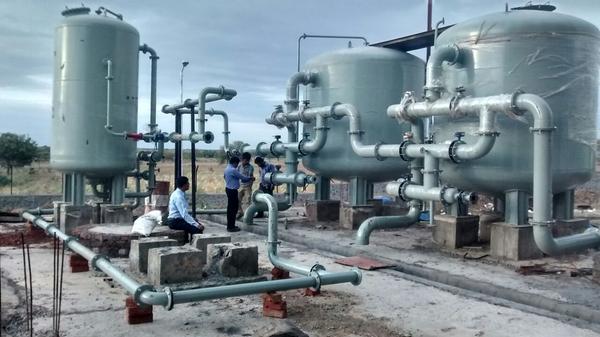
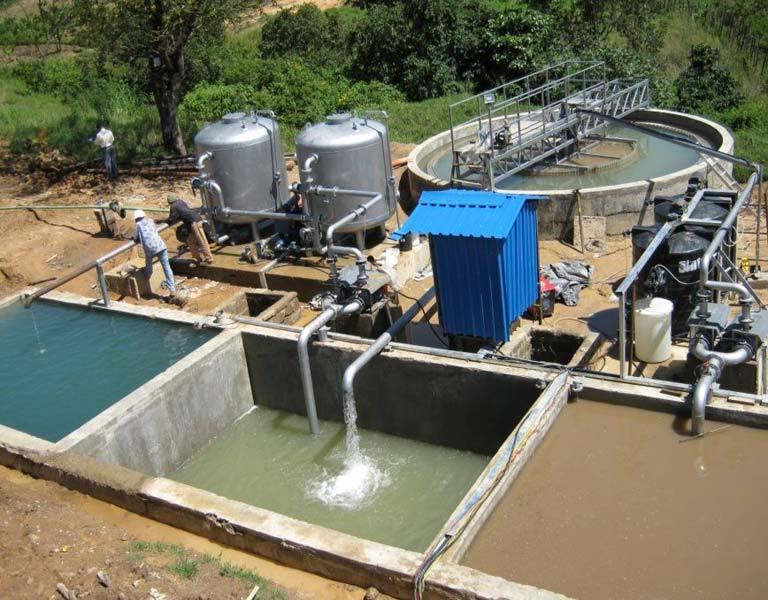
A Water Treatment Plant (WTP) is a facility designed to purify raw water (from rivers, lakes, borewells, etc.) and make it safe for drinking, industrial use, or other purposes. The goal is to remove physical, chemical, and biological impurities to meet water quality standards for a specific end-use.
The end use may be drinking, industrial water supply, irrigation, river flow maintenance, water recreation or many other uses, including being safely returned to the environment. Water treatment removes contaminants and undesirable components, or reduces their concentration so that the water becomes fit for its desired end-use. This treatment is crucial to human health and allows humans to benefit from both drinking and irrigation use.
For the elimination of hazardous chemicals from the water, many treatment procedures have been applied.
The processes involved in removing the contaminants includes:
Main Processes in a Water Treatment Plant
(a) Screening
Removes large floating objects like leaves, sticks, plastics, etc.
(b) Coagulation & Flocculation
Alum, ferric chloride, or polymers are added to clump fine suspended particles into larger “flocs.”
(c) Sedimentation
Water is kept in a tank where heavy flocs settle at the bottom.
(d) Filtration
Water passes through layers of sand, gravel, or activated carbon filters to remove smaller particles, turbidity, and color.
(e) Disinfection
Chlorine, ozone, or UV treatment kills bacteria, viruses, and pathogens.
(f) pH Correction
Lime or other chemicals are added if water is too acidic or alkaline.
Advanced Treatment (Optional)
Reverse Osmosis (RO): Removes dissolved salts and minerals.
Ultrafiltration (UF): Removes finer particles and microorganisms.
Activated Carbon Filters: Remove odor, taste, pesticides, organic matter.
Ion Exchange / Softening: Removes hardness (calcium & magnesium).
The key properties that define a WTP:
Multi-stage treatment processes:
WTPs employ a series of physical, chemical, and sometimes biological processes to eliminate a wide range of contaminants.
Common processes include:
Coagulation and Flocculation: Chemicals are added to clump small particles into larger flocs.
Sedimentation: Flocs settle out of the water due to gravity.
Filtration: Water passes through filters to remove remaining suspended solids and some microorganisms.
Disinfection: Chemicals like chlorine or UV light are used to kill harmful bacteria, viruses, and pathogens.
pH Adjustment: Adjusting the acidity or alkalinity of the water for optimal treatment and safety.
Advanced treatment methods like Reverse Osmosis (RO), Ultrafiltration (UF), and Nanofiltration (NF) may also be integrated depending on the specific water source and required water quality.
Water quality monitoring and control:
WTPs continuously monitor and analyze various water quality parameters throughout the treatment process to ensure the final output meets regulatory standards and intended uses.
Key parameters include: pH, turbidity, Total Dissolved Solids (TDS), hardness, the presence of microorganisms, and levels of specific chemicals.
Automated sensors and data analysis are increasingly utilized for real-time monitoring and process optimization.
Adaptability and flexibility:
WTPs are designed to adapt to variations in raw water quality and demand fluctuations.
Factors considered in design include the source water's characteristics, required capacity, and potential for future expansion.
The selection of treatment technologies and plant size are tailored to address the unique challenges of the water source and intended use.
Sludge and waste management:
Water treatment processes generate sludge and other waste materials that require proper handling and disposal to minimize environmental impact.
Sludge treatment and dewatering systems are an integral part of WTPs to ensure safe and compliant disposal.
Some WTPs are implementing advanced solutions like Zero Liquid Discharge (ZLD) to maximize water reuse and minimize waste generation.
Automation and efficiency:
Modern WTPs incorporate automation and control systems, including PLCs and SCADA, to enhance efficiency, reduce operating costs, and improve reliability.
These systems enable remote monitoring, automated process adjustments, and data logging for optimal performance and maintenance.
Energy efficiency is also a key consideration in WTP design and operation, with technologies like gravity-fed systems and solar-powered pumps being explored for sustainable practices.
Safety and regulatory compliance:
WTPs are designed and operated in adherence to strict safety standards and regulatory guidelines set by organizations like the World Health Organization (WHO) and local regulatory bodies.
This ensures the safety of the treated water, prevents environmental pollution, and minimizes potential health risks.
By effectively managing these key properties, WTPs play a crucial role in safeguarding public health, protecting the environment, and ensuring the availability of this vital resource for future generations.
* Major Components of a WTP
Intake well & raw water pump house
Screens & grit chambers
Flash mixer & flocculator
Clarifier (sedimentation tank)
Rapid sand filters / Pressure filters
Disinfection unit (chlorination, UV, ozone)
Treated water storage & distribution system
* Applications
Municipal drinking water supply
Industrial process water (power plants, textiles, pharma, food processing, etc.)
Hotels, hospitals, and commercial complexes
Irrigation & agricultural use
* Benefits
✅ Provides safe, potable water
✅ Prevents waterborne diseases (typhoid, cholera, dysentery)
✅ Removes harmful chemicals (arsenic, fluoride, nitrates)
✅ Improves water taste, odor, and clarity
✅ Meets environmental and regulatory standards
The sequencing batch reactor (SBR) is a fill-and- draw activated sludge system for wastewater treatment. In this system, wastewater is added to a single “batch” reactor, treated to remove undesirable components.
A Sequencing Batch Reactor (SBR) is a type of activated sludge wastewater treatment system that utilizes a fill-and-draw process where all stages of treatment occur sequentially in a single tank. Unlike conventional continuous flow systems that require separate tanks for each process (e.g., equalization, aeration, clarification), SBRs integrate these stages into a single reactor operated in a timed sequence.
How SBR wastewater treatment works
The SBR treatment cycle typically consists of five sequential phases:
Fill: Wastewater is pumped into the SBR tank, where it mixes with the activated sludge (biomass) from the previous cycle.
React: Air is supplied to the tank via an aeration system, providing oxygen for the microorganisms to break down organic pollutants (BOD, ammonia, nitrogen).
Settle: Aeration stops, allowing the activated sludge to settle at the bottom of the tank due to gravity, leaving clear, treated water above.
Decant: The clear, treated water (supernatant) is removed from the tank without disturbing the settled sludge.
Idle: This is a waiting period before the next fill phase, during which excess sludge can be removed.
Advantages of SBR wastewater treatment
Compact Footprint: SBRs require less space compared to conventional systems as all treatment stages happen in a single tank, making them suitable for areas with limited land availability.
Operational Flexibility: SBRs are adaptable to varying flow rates and organic loads, making them suitable for industrial and municipal applications with fluctuating wastewater characteristics.
High Treatment Efficiency: SBRs can achieve high removal efficiencies for organic matter, nitrogen, and phosphorus due to the controlled aeration and anoxic/anaerobic cycles.
Nutrient Removal: SBRs can effectively remove nitrogen and phosphorus without the need for chemical addition, promoting biological nutrient removal (BNR).
Reduced Odor: Aerobic conditions throughout much of the cycle minimize odor generation compared to anaerobic systems.
Automated Operation: Modern SBR systems are highly automated, reducing the need for constant manual oversight.
Potential for Water Reuse: The high-quality effluent produced by SBRs can be suitable for various reuse applications after further disinfection and filtration.
Applications of SBR wastewater treatment
SBR technology is used in various municipal and industrial wastewater treatment settings, including:
Small to medium-sized municipal plants
Industrial applications such as food processing, pharmaceuticals, and chemical manufacturing
Remote or decentralized facilities
Upgrading existing plants
Advanced SBR systems like the Hybrid Granular SBR (GST) can improve efficiency using bio-beads that help retain biomass, leading to better removal of organic carbon, nitrogen, and phosphorus. GST systems also reduce the need for certain equipment, resulting in a smaller size and lower costs.
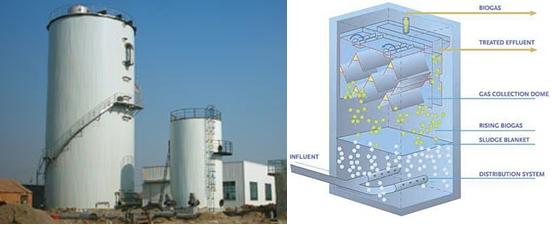
An upflow anaerobic sludge blanket (UASB) reactor is a type of anaerobic digester used for wastewater treatment, particularly for high-strength industrial wastewater. It's a single-tank process where wastewater flows upwards through a suspended blanket of granular sludge, breaking down organic pollutants and producing biogas. This technology is known for its efficiency in removing organic matter and its ability to produce usable biogas.
How it works
Wastewater inflow: Raw wastewater enters the reactor from the bottom.
Sludge blanket contact: It flows upward through a dense blanket of granular sludge (microbial aggregates).
Anaerobic degradation: Anaerobic microorganisms within the sludge blanket break down organic pollutants in the wastewater through anaerobic digestion.
Biogas production: This process generates biogas, primarily methane and carbon dioxide, which bubbles upward, providing mixing and contributing to energy recovery potential.
Phase separation: A gas-liquid-solid separator at the top of the reactor separates the treated liquid effluent, biogas, and sludge particles, returning the sludge to the digestion compartment.
Effluent discharge/post-treatment: The treated effluent, with significantly reduced organic load (BOD and COD), can then be discharged or undergo further treatment for removal of nutrients (nitrogen and phosphorus) and pathogens.
Advantages
High organic loading capacity: Capable of effectively treating wastewater with high organic loads.
Energy generation: Produces biogas (methane) as a renewable energy source that can be captured and utilized.
Low sludge production: Generates a smaller quantity of stabilized sludge compared to aerobic systems, reducing sludge handling and disposal costs.
Low energy requirements: Operates without the need for energy-intensive aeration systems common in aerobic treatments.
Low land requirements: Compact design compared to conventional systems.
Relatively simple design and operation.
Applications
UASB reactors are particularly well-suited for treating:
Industrial wastewater: Examples include wastewater from industries like breweries, distilleries, food processing, pulp and paper, and tanneries, as well as agricultural wastes.
High-strength wastewaters with high carbohydrate content.
A membrane bioreactor (MBR) is a wastewater treatment technology that combines biological treatment with membrane filtration. It uses microorganisms to break down organic pollutants and then employs membranes (like microfiltration or ultrafiltration) to separate the treated water from the remaining solids and microorganisms. This results in high-quality effluent suitable for reuse and a smaller footprint compared to traditional activated sludge systems.
How it works
Pre-treatment: Wastewater first undergoes pre-screening to remove larger debris that could damage the membranes.
Biological Degradation: The pre-treated wastewater enters a bioreactor where microorganisms break down organic pollutants. Aeration is provided to support the microbial activity.
Membrane Filtration: The biologically treated water then passes through submerged membranes (usually microfiltration or ultrafiltration) which act as a filter, separating the treated water from the mixed liquor containing the microorganisms and other solids.
Effluent & Sludge Management: The high-quality treated water (permeate) can then be reused or safely discharged. The concentrated sludge is managed, potentially undergoing further treatment or disposal.
Key advantages
High-quality effluent: MBR systems produce effluent of excellent quality, often suitable for reuse applications like irrigation or industrial processes. MBRs produce high-quality effluent with low levels of suspended solids, organic matter (COD/BOD), nutrients (nitrogen and phosphorus), and pathogens, meeting stringent environmental standards.
Smaller footprint: The MBR design eliminates the need for large secondary clarifiers, leading to a more compact treatment plant and saving space.
Enhanced treatment efficiency: MBR systems effectively remove suspended solids, organic pollutants (BOD, COD), nutrients (nitrogen, phosphorus), and pathogens.
Increased operational control: MBRs offer better control over the solids retention time (SRT) and hydraulic retention time (HRT), which allows for better management of the microbial population and overall treatment efficiency.
Reduced sludge production: MBR systems generally produce less waste activated sludge compared to conventional activated sludge processes.
Applications
MBR technology is suitable for treating various types of wastewater, including:
Municipal wastewater: Widely used in municipal wastewater treatment plants, especially in areas with limited space or stringent discharge regulations.
Industrial wastewater: Effective in treating industrial effluents, including those with high organic loads and difficult-to-degrade substances (e.g., from food and beverage, pharmaceutical, and petrochemical industries).
Landfill leachate: Used for treating landfill leachates which contain a wide range of organic and inorganic compounds.
MBR wastewater treatment stands for Membrane Bioreactor wastewater treatment, which is a state-of-the-art method that combines conventional activated sludge (biological treatment) with advanced membrane filtration.
Water softeners are filtration systems designed to tackle the problem of hard water, which is water with a high concentration of dissolved minerals like calcium and magnesium. These minerals are picked up as water flows through rock and soil deposits.
How water softeners work to address this issue:
Ion Exchange: Most water softeners use ion exchange, where hard water passes through resin beads that swap sodium ions for calcium and magnesium ions.
Regeneration: When the resin is full of hard minerals, a saltwater solution is used to flush out the minerals and replenish the sodium ions.
Why water softening is important
Hard water can cause problems:
Scale Buildup: It creates limescale in pipes and appliances, reducing efficiency and lifespan.
Reduced Cleaning Efficiency: Hard water makes soaps and detergents less effective.
Damaged Appliances: Scale can shorten the life of appliances.
Higher Energy Consumption: Scale on heating elements increases energy use.
Using water softeners can prevent these issues, leading to benefits such as:
Extended Lifespan: Protects plumbing and appliances.
Improved Cleaning: Makes soaps work better.
Better Skin and Hair: Gentler on skin and hair.
Increased Efficiency: Appliances run more efficiently.
Cost Savings: Reduces bills and replacement costs.
Water softeners are important in water treatment for improving water quality and protecting systems from hard water's effects.
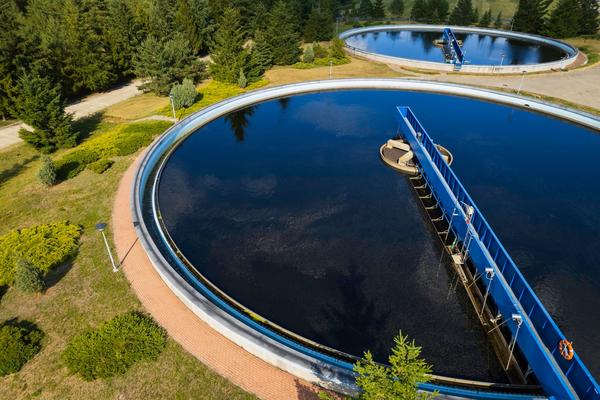
A sewage treatment plant (STP) is a facility that treats wastewater, primarily from domestic and commercial sources, to remove contaminants and pollutants before releasing it back into the environment. These plants play a crucial role in public health, water quality, and ecosystem preservation by ensuring wastewater is treated and purified.
How STPs work: 'a multi-stage process'
STPs employ a combination of physical, biological, and sometimes chemical processes, typically involving three main stages:
Preliminary Treatment: This initial stage focuses on removing large debris and heavy solids that could damage equipment or obstruct the flow. This is achieved through screening (using bar screens) and grit removal in grit chambers.
Primary Treatment: In this stage, wastewater flows into large sedimentation tanks where heavier solids settle to the bottom, forming primary sludge, while lighter materials like grease and oil float to the surface and are skimmed off. This stage removes a significant portion of suspended solids and organic matter.
Secondary Treatment: This involves biological processes, primarily using microorganisms (bacteria and protozoa) to break down dissolved and suspended organic matter that remained after primary treatment. This is often carried out in aeration tanks where air is introduced to promote the growth of these microorganisms, creating activated sludge, which then settles out in a secondary clarifier. This process can significantly reduce organic matter and pathogens.
Tertiary Treatment: This advanced stage, often optional but crucial for specific applications or sensitive environments, aims for further purification. It may involve filtration to remove finer particles, disinfection (using chlorine, ultraviolet light, or ozone) to eliminate remaining pathogens, and nutrient removal (nitrogen and phosphorus) to prevent eutrophication.
Sludge Treatment:
The sludge generated from primary and secondary treatment undergoes further processing, such as dewatering and drying, and may be used as fertilizer after undergoing stabilization processes
Importance and benefits of sewage treatment
Environmental Protection: STPs prevent water pollution by removing harmful contaminants from wastewater before it's discharged into rivers, lakes, and oceans, protecting aquatic life and maintaining ecosystem balance.
Public Health Protection: By eliminating pathogens and toxins, STPs reduce the risk of waterborne diseases like cholera, typhoid, and dysentery.
Water Reuse and Conservation: Treated wastewater can be safely reused for various non-potable purposes such as irrigation, industrial cooling, toilet flushing, and groundwater recharge, reducing the reliance on freshwater resources.
Resource Recovery: Some STPs can recover valuable resources like biogas (a renewable energy source) from sludge digestion, and nutrients like nitrogen and phosphorus, which can be used as fertilizers.
Regulatory Compliance: STPs help industries and municipalities meet strict wastewater discharge regulations, avoiding fines and legal issues.
Our Expertise:
- Customized STP design and installation
- Advanced treatment technologies: physical, chemical, and biological processes
- Effective removal of pollutants and contaminants: BOD, COD, TSS, pH, etc.
- Compliance with environmental regulations: CPCB, MPCB, etc.
- Regular maintenance and operation support
Benefits of Our STP Solutions:
- Reduced environmental impact
- Compliance with regulatory requirements
- Cost savings through water reuse and recycling
- Improved public health and hygiene
- Enhanced community reputation and social responsibility
Effluent Treatment Plant (ETP)
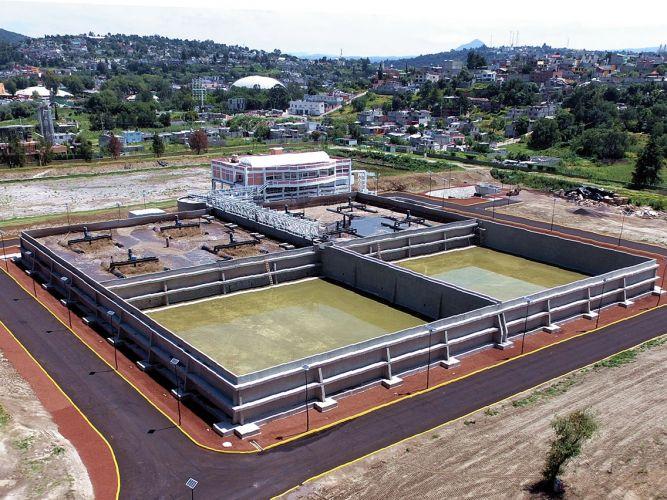
SK Enterprises offers innovative and effective Effluent Treatment Plant (ETP) solutions to manage industrial wastewater and ensure environmental compliance. An Effluent Treatment Plant (ETP) or Waste Water Treatment Plant (WWTP) is a unit plant where various physical, biological and chemical processes are used to change the properties of the waste water by removing harmful substances in order to turn it into hazard free water.
An Effluent Treatment Plant (ETP) that treats industrial wastewater to remove contaminants and pollutants before discharge into the environment or for reuse. ETPs employ a combination of physical, chemical, and biological processes to purify the water, ensuring it meets environmental standards and minimizes harm to ecosystems.
Key aspects of Effluent Treatment Plants:
Purpose:
ETPs are designed to treat wastewater generated by various industries, including textiles, pharmaceuticals, chemicals, and food processing, which can contain a wide range of pollutants.
Treatment Processes:
ETPs utilize a multi-stage treatment process, which may include:
Preliminary Treatment: Removing large debris, grit, and other solids.
Primary Treatment: Utilizing physical and chemical processes like coagulation and flocculation to remove suspended solids and some dissolved pollutants.
Secondary Treatment: Employing biological processes, such as the activated sludge process, to break down organic matter using microorganisms.
Tertiary Treatment: Implementing advanced filtration, disinfection, and other methods to remove remaining pollutants and pathogens.
Sludge Handling: Collecting, treating (thickening, dewatering, digestion), and disposing of the solid by-product (sludge) in an environmentally responsible manner.
Importance:
ETPs are crucial for:
Protecting water resources from contamination.
Complying with environmental regulations and avoiding penalties.
Enabling the safe reuse of treated water for non-potable purposes within the industry or for irrigation.
Reducing the environmental impact of industrial wastewater discharge.
Industry Applications:
ETPs are widely used in various industries, including:
-Textile
-Chemical
-Pharmaceutical
-Food processing
-Refineries
-Dairy
-Leather
Our ETP Solutions:
- Customized ETP design and installation
- Advanced treatment technologies: physical, chemical, and biological processes
- Effective removal of pollutants and contaminants: BOD, COD, TSS, pH, etc.
- Compliance with environmental regulations: CPCB, MPCB, etc.
- Regular maintenance and operation support
Benefits of Our ETP Solutions:
- Reduced environmental impact
- Compliance with regulatory requirements
- Cost savings through water reuse and recycling
- Improved brand reputation and social responsibility
- Enhanced employee safety and health
 Chat with us
 Chat with us